
Views: 0 Author: Site Editor Publish Time: 2026-10-12 Origin: Site


Supply chain and operations managers know the hard truth about packaging logistics. Securing high-quality empty containers is only half the battle. Preventing transit damage, contamination, and feeding issues during the final mile is where you truly protect margins. Empty, unpressurized aluminum packaging remains incredibly vulnerable during transit. They easily succumb to crushing forces, scuffing vibrations, and environmental factors like sudden humidity shifts. If you ignore these logistical risks, your production lines will suffer from unexpected downtime and material waste.
We designed this guide as a comprehensive technical checklist for facility readiness. Proper inbound logistics and receiving protocols directly protect your production timelines. They also safeguard your final product integrity before the liquid ever enters the container. By mastering these final-mile details, you ensure your packaging arrives ready for the filler. You will learn how to optimize warehouse environments, adjust for unique form factors, and audit your supply partners effectively. Let us dive into the operational steps you need to secure your supply chain.
Empty aluminum cans require strict environmental controls (temperature and humidity) to prevent condensation and oxidation prior to filling.
Site readiness dictates that unloading docks, forklift equipment, and depalletizing lines are calibrated specifically for lightweight, unpressurized pallets.
Handling protocols must adapt to form factors; a sleek aluminum can requires different load stability and line-feeding considerations than a standard format.
Evaluating an OEM packaging partner requires auditing their palletizing standards, dunnage materials, and stretch-wrapping protocols to guarantee pristine delivery.
Let us frame the business problem directly. Poor handling leads directly to significant operational losses. When empty packaging arrives damaged, you face cascading failures on the factory floor. Dented flanges cause immediate line jams at the depalletizer. Scuffed artwork ruins retail appeal and forces finished product waste. Compromised internal coatings lead to eventual seamer failures, leaks, and beverage spoilage on retail shelves.
You must understand the inherent vulnerability of unfilled packaging. Without internal pressure, empty containers lack both axial and radial crush strength. They behave almost like fragile eggshells. Until the filler drops liquid inside and the seamer locks the lid in place, the thin metal cylinder cannot withstand heavy lateral or vertical pressure. A slight bump from a careless forklift blade can ruin an entire tier in seconds. Once a single row collapses, the structural integrity of the entire pallet fails.
To combat this, facilities must define strict Acceptable Quality Limit (AQL) criteria upon delivery. Standard acceptable defect rates generally hover below 0.1% for empty beverage packaging deliveries. When shipments exceed this threshold, operators need a clear action plan. Always document transit damage immediately. Take clear, well-lit photographs before unloading the truck. This visual evidence prevents costly disputes when you file claims against freight carriers or suppliers. Standardize this documentation process to protect your operational budget.
Your receiving bays dictate the overall success of your inbound logistics. We must outline specific physical requirements for unloading zones. Level dock plates are absolutely non-negotiable. Uneven transition plates cause lightweight pallets to rock violently as forklifts cross them. This rocking momentum easily tips the top tiers onto the dock floor. You also need specialized forklift equipment for safe handling. Standard forklift blades often pinch or tilt fragile loads. We highly recommend using hydraulic side-shifters. Widened forks also help distribute the pallet weight evenly across the entire base, preventing middle-sag.
Warehousing environmental controls present another critical hurdle for site readiness. Keep your storage areas bone dry and rigorously temperature-controlled. Sudden temperature swings cause "sweating" or rapid condensation on the bare metal. This moisture compromises the internal epoxy lining. It also causes external water stains that ruin the aesthetic of the final product. Maintaining a steady dew point is mandatory for long-term storage.
Pest and hygiene controls are equally vital for regulatory compliance. You must maintain strict food-safety compliance at all times. Adhere tightly to FDA and GFSI (Global Food Safety Initiative) standards. These standards require fully sealed warehouse environments. You must strictly separate empty beverage containers from raw agricultural materials, allergens, or strong-smelling chemicals. Airborne contaminants easily settle inside open containers, creating severe safety risks.
We also need to address physical stacking limitations. Double-stacking saves warehouse space but introduces severe structural risks. You must follow strict guidelines based on floor grading and pallet weight distribution.
Table 1: Environmental and Stacking Guidelines for Empty Pallets
Category | Standard Requirement | Risks of Non-Compliance |
|---|---|---|
Temperature | 65°F - 75°F (18°C - 24°C) | Condensation, moisture buildup on internal epoxy lining. |
Humidity | Below 60% Relative Humidity | External oxidation, dulling of graphics, bacterial growth. |
Floor Grade | Less than 1% slope | Pallet leaning, top-tier tipping, catastrophic load failure. |
Stacking Height | Max 2 pallets (only if fully banded) | Lower tier crushing, loss of total structural integrity. |
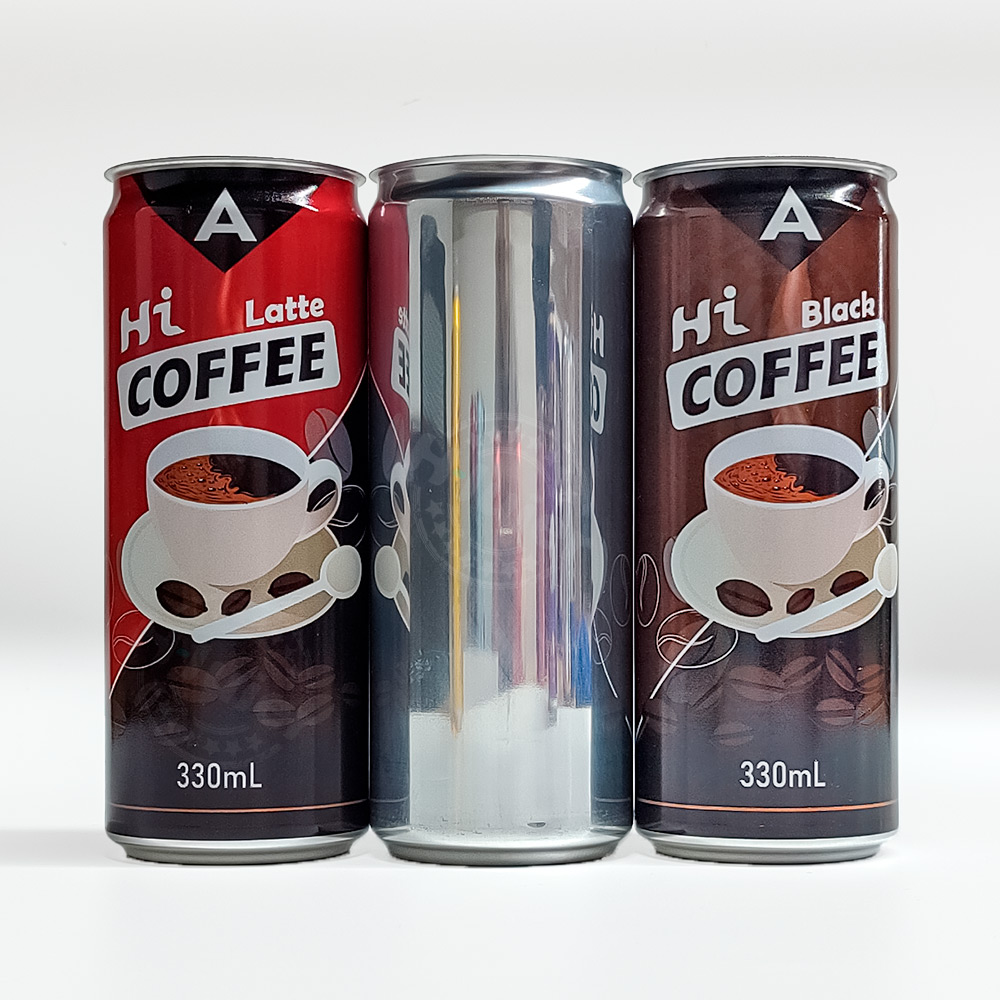
Establishing robust standard operating procedures (SOPs) is essential for any production facility. Proper custom aluminum cans handling from the inbound truck to the warehouse floor protects your bottom line. Every operator must understand they are moving highly engineered, fragile components. Training your forklift drivers specifically for unpressurized loads reduces daily damage rates significantly.
Follow these sequential SOPs for moving pallets safely:
Set strict forklift speed limits inside the receiving zone, keeping movement below 3 mph.
Train drivers on smooth acceleration and gentle braking to prevent sudden momentum shifts.
Avoid sharp turns entirely, as lateral G-forces cause top-heavy loads to lean and shift.
Lower the pallet as close to the warehouse floor as physically possible during transit.
Inspect the pallet base for broken wooden slats before attempting to lift the load.
Dunnage and slip sheets play a critical role in load stability. Pallets require high-quality chipboard or plastic slip sheets between every single tier. These tier sheets distribute vertical weight evenly across the rims of the containers below. They also prevent aggressive metal-on-metal friction. Friction generates fine aluminum dust during transit. This microscopic dust clogs depalletizer optical sensors and contaminates the sterile fill zone.
Next, you must evaluate your depalletizing readiness. You must stage pallets correctly before feeding the line. Never move a pallet straight from a cold delivery truck into a warm, humid filling room. Include a mandatory acclimatization period in your workflow. Bring the containers to ambient room temperature first. This simple staging step prevents sudden condensation during the cold-fill process. If you fill cold liquid into a sweating container, you risk severe seaming defects and label adhesion failures.
Handling protocols must change based on the specific physical dimensions of the container. A sleek aluminum can demands highly specialized logistics compared to a standard 12 oz format. You cannot treat different geometries with the same handling procedures.
The taller, narrower profile completely shifts the center of gravity. Sleek formats create a significantly higher center of gravity on a fully loaded pallet. This physical trait makes them much more susceptible to tipping during over-the-road transit. It also increases the risk of leaning during normal forklift movement across dock plates. Operators must corner slower and brake softer when handling sleek formats to maintain absolute vertical alignment.
Suppliers must also adjust their tension and wrapping protocols accordingly. Standard stretch-wrap tension will easily crush the outer rows of a sleek pallet. The narrow diameter simply offers less radial resistance against the plastic film. Suppliers must calibrate their automated wrap tension precisely. They must also use heavy-duty corner boarding along all four edges. This rigid boarding ensures load stability without squeezing the delicate perimeter columns inward.
Line changeovers require specific mechanical adjustments too. When switching between standard and sleek formats, operators must adjust the depalletizer sweep height carefully. They must also narrow the conveyor guide rails downstream. If you fail to adjust the guide rails, the narrower containers will bounce, bottleneck, and bridge across the belt. This bridging ultimately causes them to crush under continuous line pressure.
Table 2: Standard vs. Sleek Format Adjustments
Handling Factor | Standard Format | Sleek Format |
|---|---|---|
Center of Gravity | Moderate; evenly distributed base | High; top-heavy on full pallets |
Wrap Tension | Standard factory tension limits | Reduced tension with rigid corner boards |
Conveyor Rails | Standard width settings | Narrowed settings to prevent bridging |
Depalletizer Sweep | Standard height calibration | Lowered calibration for taller profiles |
Visual appeal directly drives consumer purchasing decisions on retail shelves. A damaged exterior ruins the entire marketing and branding effort. We must address the specific vulnerabilities of a printed beverage can. These decorated containers undergo extreme mechanical stress during over-the-road transit.
Micro-vibrations occur constantly during freight transport. These high-frequency vibrations cause adjacent containers to rub against each other thousands of times per hour. This continuous friction creates severe scuffing risks. It easily dulls premium matte varnishes. It also aggressively scratches high-gloss UV inks. If a delivery truck has poor air suspension, the resulting friction can destroy an entire pallet's aesthetic value before it ever reaches your dock.
Top-tier suppliers use advanced packaging solutions to mitigate this exact rubbing risk. They employ high-tension vertical banding systems that compress the load securely. They use rigid wooden or plastic top frames to hold the upper tiers perfectly square. They also optimize tier-sheet materials to gently grip the rims, effectively locking the cylinders in place. When containers cannot vibrate laterally against one another, they simply cannot scuff.
Your quality assurance (QA) teams need strict, repeatable inspection protocols. They should visually inspect the outer perimeter of a pallet before ever signing the bill of lading (BOL). The outer rows represent the absolute highest risk zone for transit scuffing and strap damage. If QA spots rubbed ink, dull patches, or exposed bare metal, they must flag the shipment immediately for quarantine and review.
Choosing the right manufacturing partner mitigates most handling risks before they even start. A reliable OEM aluminum can manufacturer is not evaluated solely on their unit cost. You must deeply evaluate their outbound logistics competency. If they manufacture a perfect product but ship it poorly, your factory absorbs all the resulting waste and downtime.
You need to ask targeted, operational questions during the initial auditing process. Do not rely on sales brochures. Dig into their actual warehouse procedures. Use this checklist when interviewing potential suppliers:
What are your standard pallet configurations, and what are your maximum height limits for export?
Do you use automated strapping and wrapping machines to ensure consistent load tension?
How often do you mechanically calibrate your stretch-wrap tensioners?
What are your specific protocols for LTL (Less Than Truckload) shipping versus dedicated FTL (Full Truckload) shipping?
Do you use dedicated top frames and edge protectors for all long-haul freight?
Take concrete action before signing any long-term volume contract. Always request a small trial shipment first. Run this trial shipment through your entire receiving, warehousing, and depalletizing sequence. Audit the supplier's packaging specifications sheet closely. Ensure their dunnage standards align perfectly with your warehouse environmental controls and forklift capabilities. Proactive auditing prevents chaotic receiving bays later.
Protecting your operational investment requires a massive mindset shift across your facility. You must train your teams to treat empty containers as highly engineered, fragile components. They remain highly vulnerable until they are successfully filled, pressurized, and fully seamed. Every single touchpoint from the supplier's loading dock to your depalletizer directly impacts your final production yield.
Operations and procurement teams need to act immediately. Review your site readiness today. Inspect your dock levelers, calibrate your forklift attachments, and rigorously check your warehouse climate controls. Partner with a packaging supplier that engineers their delivery process just as rigorously as their manufacturing process. When you secure your inbound logistics protocols, your production lines will run flawlessly.
A: You can typically double-stack fully banded pallets if your warehouse floor has less than a 1% slope. Single stacking is highly recommended for long-term storage or if the warehouse experiences high forklift traffic. Never double-stack unbanded or partial pallets, as the lack of structural integrity will cause the bottom load to crush immediately.
A: We strongly recommend using empty containers within 3 to 6 months. While aluminum itself does not degrade quickly, the internal epoxy liners can dry out or absorb moisture over time. Prolonged exposure to high humidity also causes external oxidation, which ruins printed graphics and impacts final seaming quality.
A: Less Than Truckload (LTL) shipping involves frequent terminal cross-docking, which drastically increases damage risks. To prevent crushing, request extreme protective crating or heavy-duty edge protectors for smaller MOQs. For the best results, we always recommend dedicated Full Truckload (FTL) shipping, as it completely bypasses intermediate transfers.
A: Quarantine the affected pallet immediately before depalletizing. Document the specific location and type of damage using timestamped photographs. Note the exact damage on the Bill of Lading (BOL) before the truck driver leaves. Finally, contact your freight carrier and supplier simultaneously to initiate a formal claim and request replacement stock.


